MJF 3D printing
Multi Jet Fusion in PA12.
MJF 3D printing at Swiss3D: functional parts and series in PA12, grey or black, without support structures, in 7–10 working days. Upload a CAD file and get price and delivery date in seconds.
- Lead time 7–10 working days
- Build volume up to 284 × 350 × 350 mm
- Tolerance ±0.3%
- No support structures
How Multi Jet Fusion works.
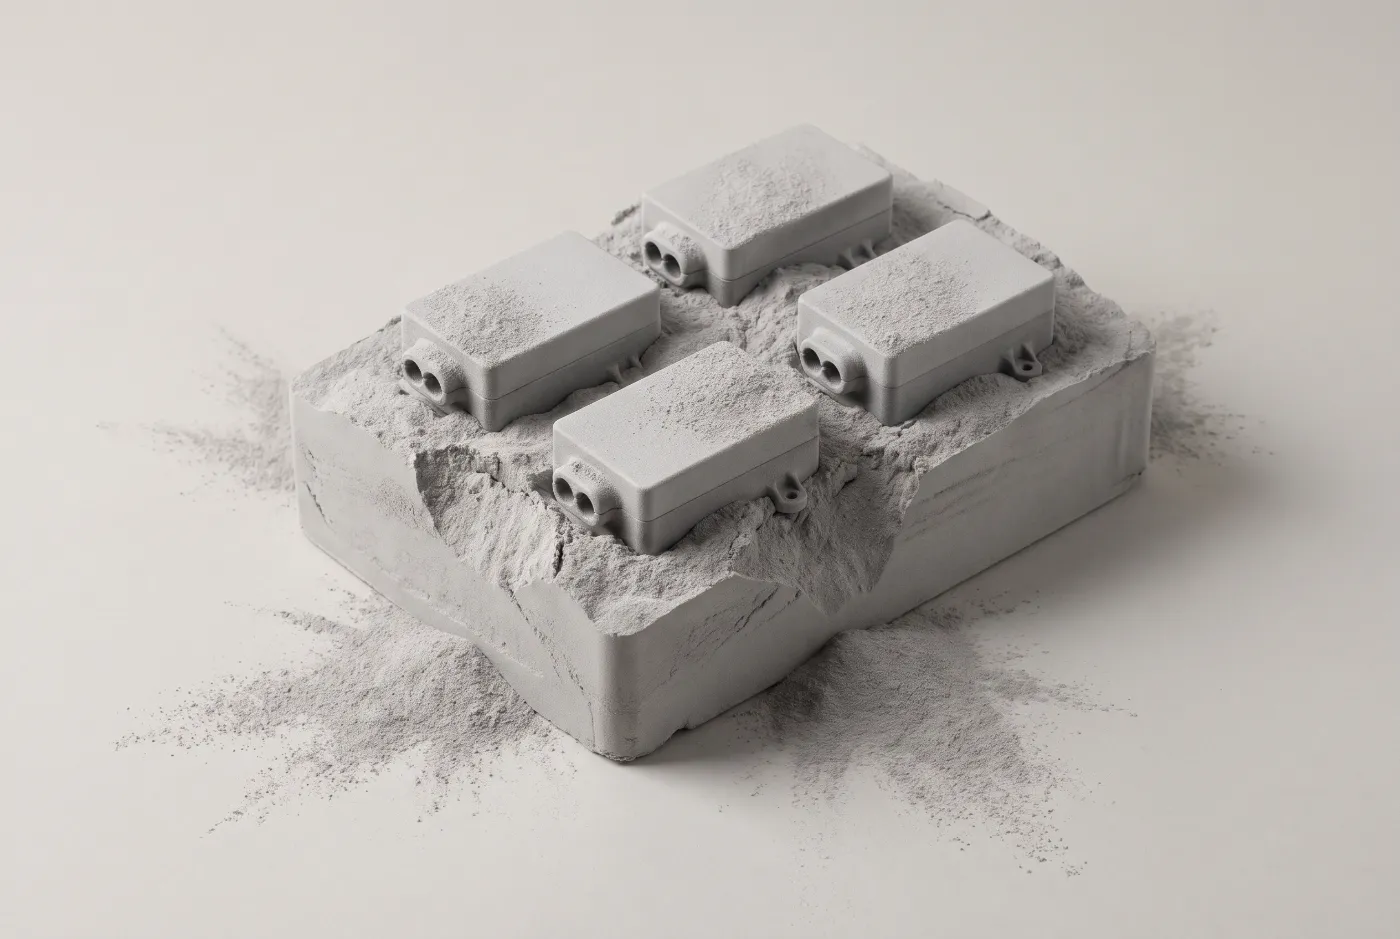
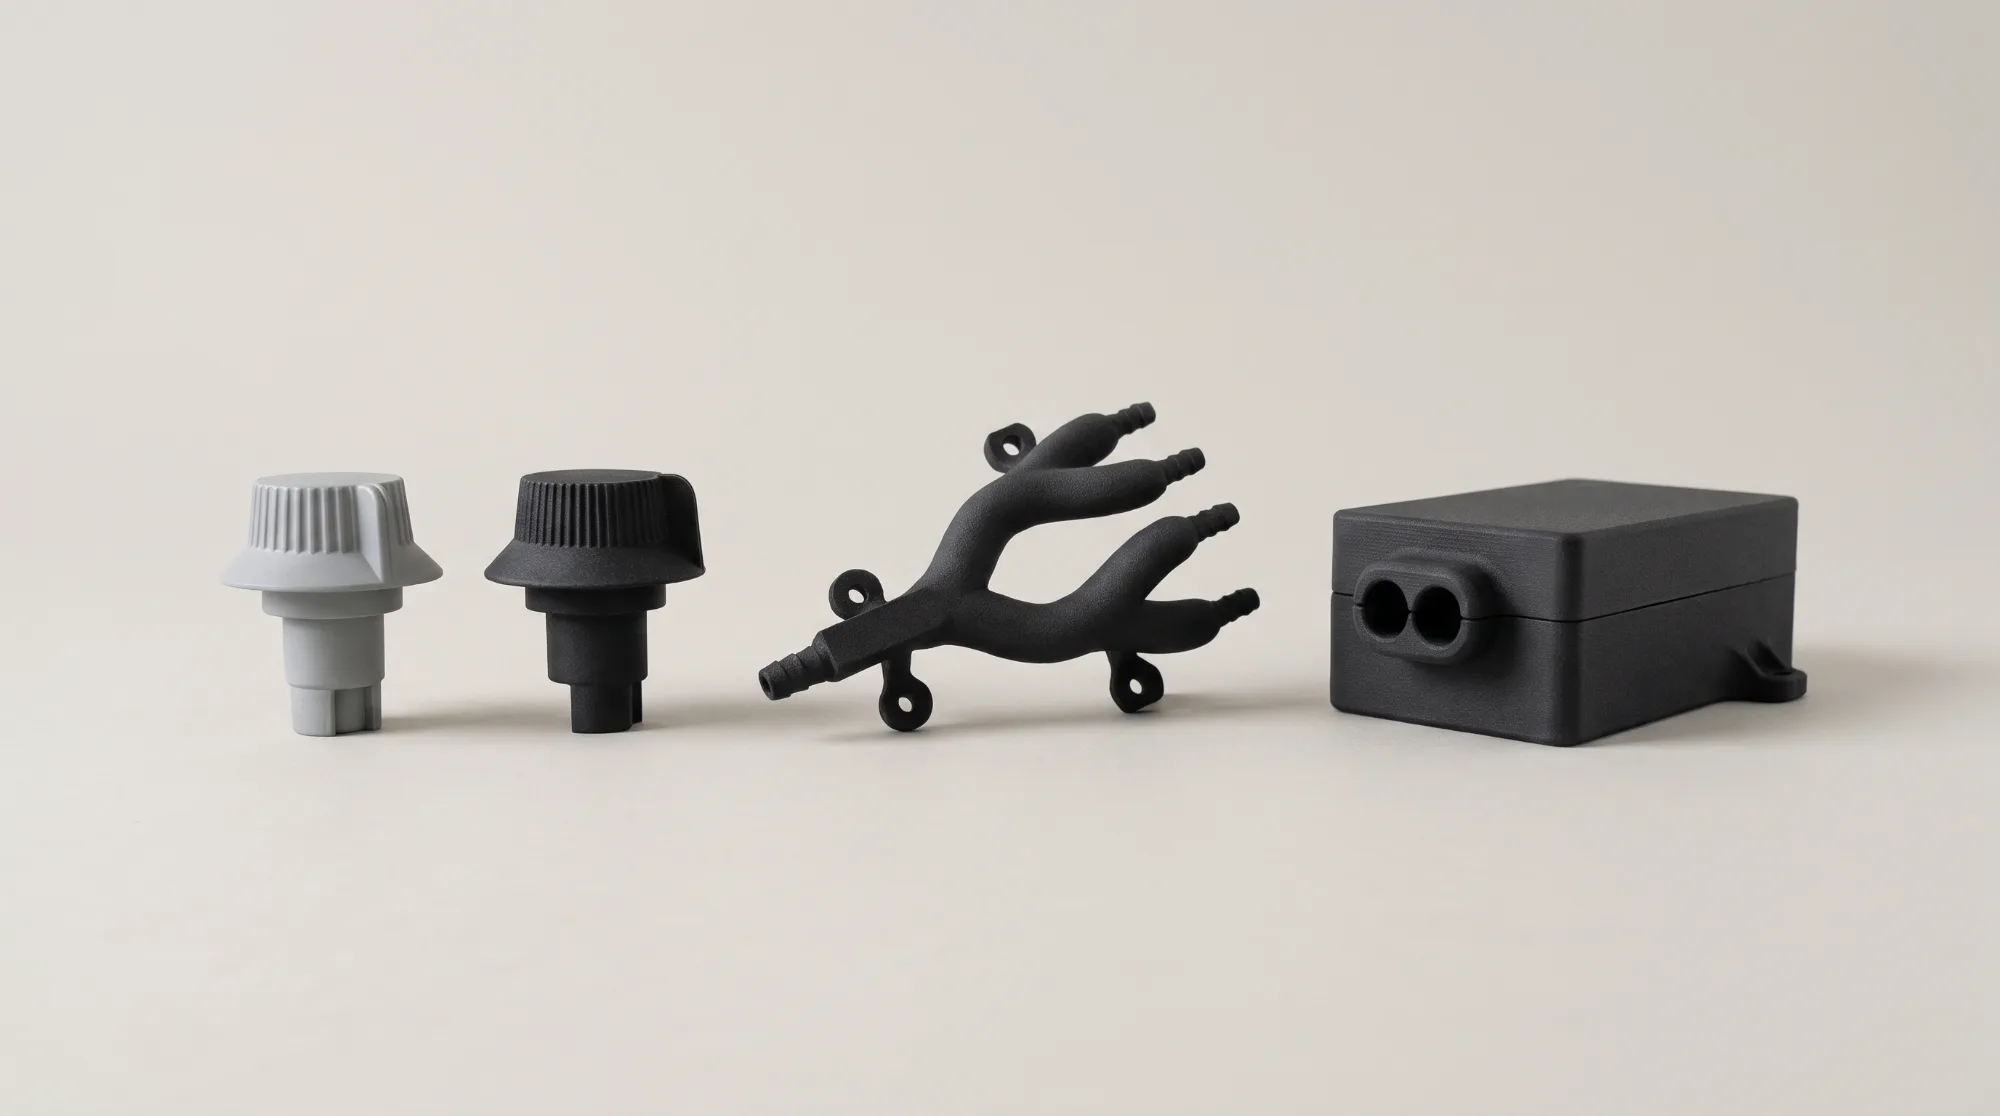
MJF 3D printing (Multi Jet Fusion) is a powder bed process developed by HP for PA12 parts. A print head applies fusing and detailing agents to each powder layer, then infrared light heats the whole layer and the powder fuses where the fusing agent lies. The resulting parts are strong and need no support structures.
The build unit is filled with PA12 powder layer by layer, each layer 0.08 mm thick. Where the fusing agent lies, the powder absorbs the heat of the infrared lamps and fuses. The detailing agent along the contours limits the heat and keeps edges and fine details clean. The loose powder around the parts supports them. MJF therefore needs no supports, and many parts can be stacked in the build volume.
After printing, the whole block cools down slowly. The parts are then depowdered, cleaned and delivered in their natural grey or dyed black. Because each layer is heated at once rather than point by point as in laser sintering, MJF is particularly suited to many identical parts with uniform properties in all directions.
MJF material PA12 and alternatives.
MJF parts are made from PA12, a tough polyamide for functional parts. For stiffer, elastic or white parts, there is the related SLS process.
All materials in the Material FinderMJF PA12
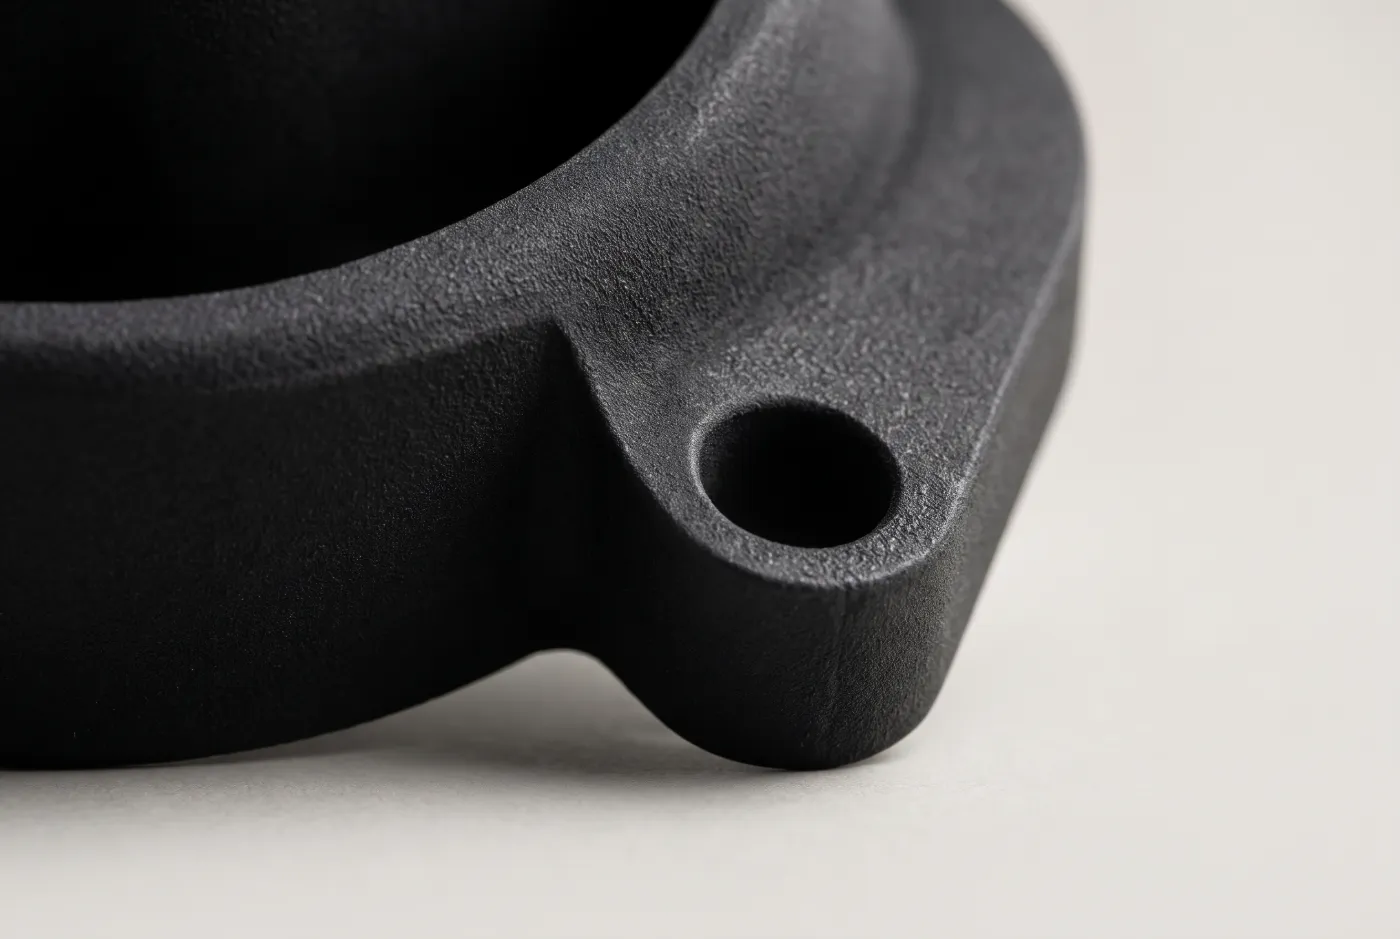
Tough polyamide 12 in grey or black. Tensile strength 46 MPa, elongation at break 36%, heat deflection temperature 145 °C at 0.45 MPa. Resistant to oils and greases.SLS PA12
The same base material in the SLS process: also in white, build volume up to 700 × 380 × 580 mm, dark grey up to 165 × 165 × 300 mm in 2–5 working days.SLS PA12-GF
Filled with glass beads, stiffer and with significantly less warping, for parts that must stay dimensionally accurate. White, up to 330 × 330 × 380 mm.SLS TPU 88A
Flexible and rubber-like, for durable elastic parts with complex geometry. Natural white.
Technical data for MJF.
Values for MJF PA12, the material of all MJF parts.
Material
PA12 (polyamide 12), melting point 183 °CColours
Grey (natural) or dyed blackBuild volume
Up to 284 × 350 × 350 mmLayer thickness
0.08 mmTolerance
±0.3%Tensile strength
46 MPa, tensile modulus 1600 MPaElongation at break
36%Heat deflection temperature
145 °C at 0.45 MPa, 82 °C at 1.8 MPaChemical resistance
Resistant to oils and greases, limited resistance to weak acids and alkalisLead time
7–10 working days (standard)Datasheet
PA12 (MJF), PDF in German with all values
Mechanical values are typical manufacturer data measured on standard test specimens, not guaranteed properties. Accuracy and strength depend on geometry and orientation in the build volume.
Information as of: November 2026
MJF for series and functional parts.
MJF rather than SLS pays off for many identical parts that carry loads and should look uniform in grey or black. For white parts, large parts or urgent single parts in dark grey, SLS is the better fit.
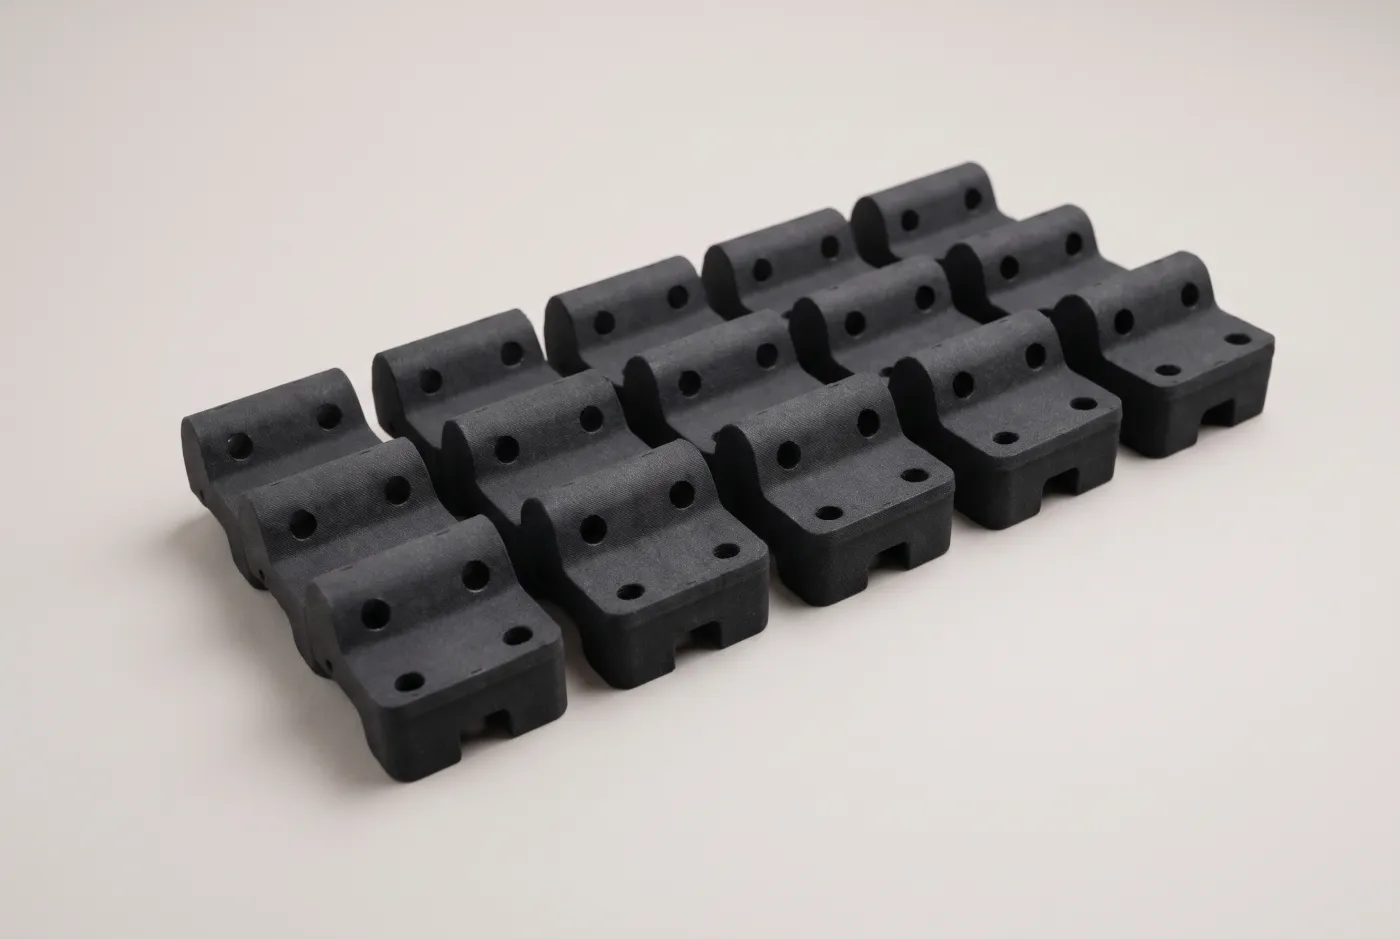
Small and medium series
Many parts are built at the same time in one build volume. As quantities rise, the price per part falls, with no tooling costs.Housings and covers
Robust housings for electronics and appliances, with a uniform look in black.Clips and snap fits
PA12 is tough: with 36% elongation at break it suits clips, snap hooks and connecting elements.Jigs and test fixtures
Holders, gauges and test fixtures for assembly and quality control, resistant to oils and greases.
SLS, MJF, SLA and FDM compared.
The four plastic processes side by side, with values for the standard material of each.
| Criterion | SLS | MJF | SLA | FDM |
|---|---|---|---|---|
| Principle | Laser sinters plastic powder | Infrared fuses the whole powder layer | UV light cures liquid resin | Nozzle deposits molten plastic |
| Materials | PA12, PA12-GF, TPU 88A | PA12 | Standard, clear and tough resin, DLP | Eleven, from PLA to PEEK |
| Surface | Matte, slightly grainy | Matte, fine-grained, slightly smoother | Smooth, layers barely visible | Visible layer lines |
| Accuracy | ±0.3% | ±0.3% | ±0.1–0.3%, DLP ±0.05% | ±0.2 mm to ±0.3% |
| Layer thickness | 0.1 mm | 0.08 mm | 0.05–0.1 mm | 0.1–0.25 mm |
| Strength | Tough, similar in all directions | Tough, similar in all directions | Stiff, standard resin rather brittle | Lower across the layers |
| Support structures | None, the powder supports | None, the powder supports | Always, contact points visible | On overhangs from about 45° |
| Largest parts | 700 × 380 × 580 mm | 284 × 350 × 350 mm | 1700 × 900 × 800 mm | 800 × 800 × 800 mm |
| Lead time | PA12 dark grey 2–5, otherwise 5–10 working days | 7–10 working days | 7–10 working days, DLP on request | 2–5 working days, PEEK 7–10 |
| Typical parts | Functional parts, clips, complex housings | Series parts, housings, brackets | Visual models, fine parts, clear parts | Fixtures, brackets, large prototypes |
| Cost | Medium | Medium, lower in series | Medium | Low (PLA, PETG) to high (PEEK) |
Principle
- SLS
- Laser sinters plastic powder
- MJF
- Infrared fuses the whole powder layer
- SLA
- UV light cures liquid resin
- FDM
- Nozzle deposits molten plastic
Materials
- SLS
- PA12, PA12-GF, TPU 88A
- MJF
- PA12
- SLA
- Standard, clear and tough resin, DLP
- FDM
- Eleven, from PLA to PEEK
Surface
- SLS
- Matte, slightly grainy
- MJF
- Matte, fine-grained, slightly smoother
- SLA
- Smooth, layers barely visible
- FDM
- Visible layer lines
Accuracy
- SLS
- ±0.3%
- MJF
- ±0.3%
- SLA
- ±0.1–0.3%, DLP ±0.05%
- FDM
- ±0.2 mm to ±0.3%
Layer thickness
- SLS
- 0.1 mm
- MJF
- 0.08 mm
- SLA
- 0.05–0.1 mm
- FDM
- 0.1–0.25 mm
Strength
- SLS
- Tough, similar in all directions
- MJF
- Tough, similar in all directions
- SLA
- Stiff, standard resin rather brittle
- FDM
- Lower across the layers
Support structures
- SLS
- None, the powder supports
- MJF
- None, the powder supports
- SLA
- Always, contact points visible
- FDM
- On overhangs from about 45°
Largest parts
- SLS
- 700 × 380 × 580 mm
- MJF
- 284 × 350 × 350 mm
- SLA
- 1700 × 900 × 800 mm
- FDM
- 800 × 800 × 800 mm
Lead time
- SLS
- PA12 dark grey 2–5, otherwise 5–10 working days
- MJF
- 7–10 working days
- SLA
- 7–10 working days, DLP on request
- FDM
- 2–5 working days, PEEK 7–10
Typical parts
- SLS
- Functional parts, clips, complex housings
- MJF
- Series parts, housings, brackets
- SLA
- Visual models, fine parts, clear parts
- FDM
- Fixtures, brackets, large prototypes
Cost
- SLS
- Medium
- MJF
- Medium, lower in series
- SLA
- Medium
- FDM
- Low (PLA, PETG) to high (PEEK)
Guide values for the standard materials; values for each material in the Material Finder. SLS in 2–5 working days applies to PA12 dark grey up to 165 × 165 × 300 mm.
Design rules for MJF.
Minimum dimensions for MJF PA12. Below these values, walls, struts and details are not reliably reproduced.
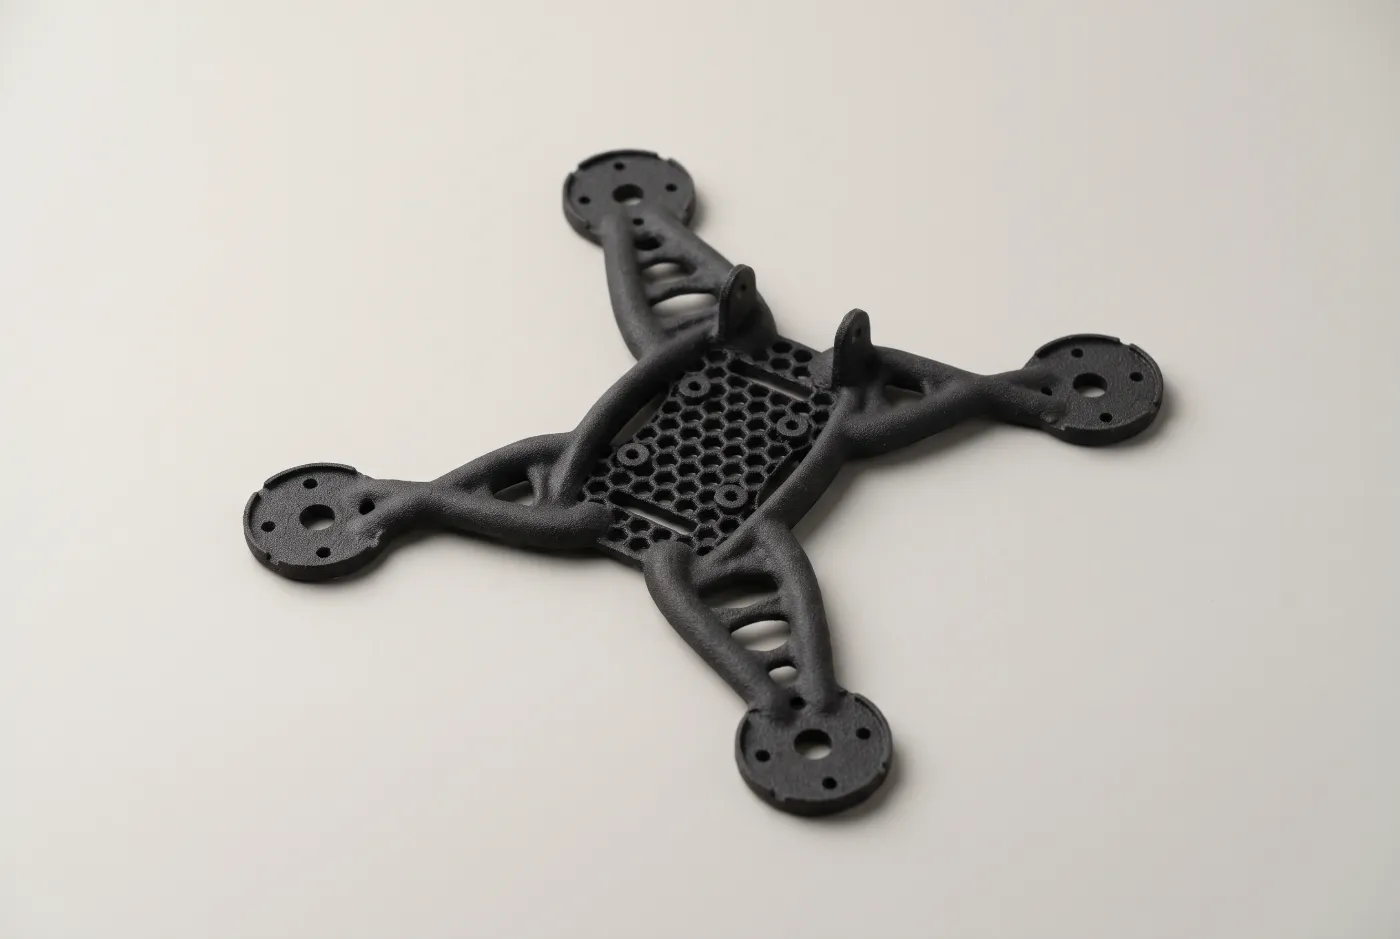
Wall thickness
From 0.6 mm for supported walls, from 0.8 mm for free-standing walls. Make load-bearing walls thicker.Struts and pins
From 0.9 mm diameter, supported or free-standing.Holes
From 0.9 mm diameter. Through holes need a clear line of sight so that all powder can be removed. In thick walls, small holes become less accurate.Details and text
Embossed and engraved from 0.4 mm.Gaps and moving parts
At least 0.6 mm between parts, walls and struts. Interlocking and moving parts can be printed in one piece.Cavities
Closed cavities stay filled with powder. For lightweight parts, provide openings for depowdering.Solid sections
Large solid cross-sections tend to warp. Hollow them out or design them with ribs.Size
Up to 284 × 350 × 350 mm in one piece. Split larger parts or print them with SLS up to 700 × 380 × 580 mm.
MJF surface finish and post-processing.
MJF parts are matt and fine-grained, smoother than SLS parts. Black, vapor smoothing and the coatings can be selected in the online quoting tool.
Grey or black
Grey is the natural colour of the powder. Dyed black, series parts look uniform, including visible parts.Vapor smoothing
Chemical smoothing with solvent vapour: a sealed, almost injection-moulded surface with less roughness and better tightness. Available for MJF parts.Coatings
Clear lacquer, UV protection and water and gas protection, each transparent, for outdoor parts or parts that must be sealed.
Alternatives to MJF 3D printing.
Single parts, white, larger parts
SLS PA12 is also available in white and up to 700 × 380 × 580 mm. Dark grey up to 165 × 165 × 300 mm in 2–5 working days.Fine details and smooth visible surfaces
SLA cures liquid resin and achieves ±0.1–0.3% depending on the resin, also transparent and paintable.Low-cost prototypes in colour
FDM is economical and available in many colours; PLA ships in 1–2 working days with express.Very large parts
Up to 800 × 800 × 800 mm with FDM, without splitting.Metal parts
Aluminium, stainless steel and titanium by laser powder bed fusion.Tight tolerances
Fits and sealing surfaces that must be tighter than ±0.3% are better milled or turned.
Frequently asked questions.
- Multi Jet Fusion is a 3D printing process developed by HP for plastic parts made from powder. A print head applies fusing and detailing agents to each powder layer, and infrared light fuses the printed areas. The loose powder supports the parts, so no support structures are needed.
- The price depends mainly on part volume, size and quantity. As quantities rise, the price per part falls. Upload your CAD file and the price appears in seconds. For single parts, compare with SLS in the same quoting tool.
- Both fuse PA12 powder without supports and reach ±0.3%. MJF has the smoother surface, thinner minimum walls (0.6 instead of 1.0 mm) and pays off for series. SLS is faster for single parts (dark grey up to 165 × 165 × 300 mm in 2–5 working days) and offers white and a build volume of up to 700 × 380 × 580 mm.
- The tolerance is ±0.3% of the dimension at a layer thickness of 0.08 mm. Details from 0.4 mm are reproduced. For tighter fits, CNC machining is the better choice.
- The standard lead time is 7–10 working days from order. After upload, the online quoting tool shows the exact delivery date. If you need parts sooner, SLS PA12 in dark grey up to 165 × 165 × 300 mm ships in 2–5 working days.
- Grey and black. Grey is the natural colour of the powder; black is achieved by dyeing and gives series a uniform look. White or light-coloured parts are available with SLS, transparent parts with SLA.
- There is no fixed threshold. MJF is designed for series parts in medium to large quantities: many parts share one build volume and the price per part falls. A single prototype is often ready sooner in dark grey SLS PA12; which process costs less depends on the shape, and the online quoting tool lets you compare both.
Price your MJF parts.
Upload a CAD file and get price and delivery date in seconds. For larger series and special requirements, send us an inquiry.
Sample images created with AI.